Factory-Engineered Systems
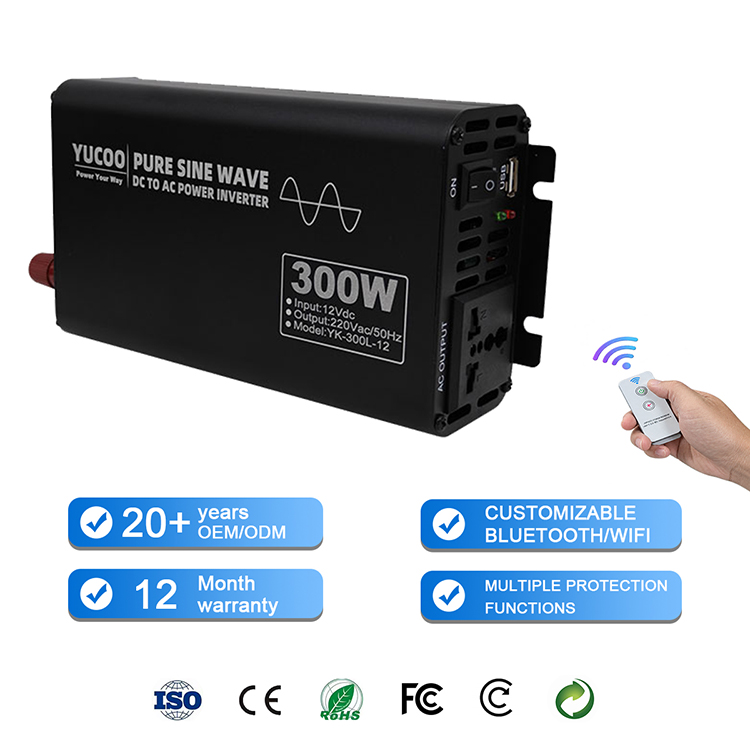
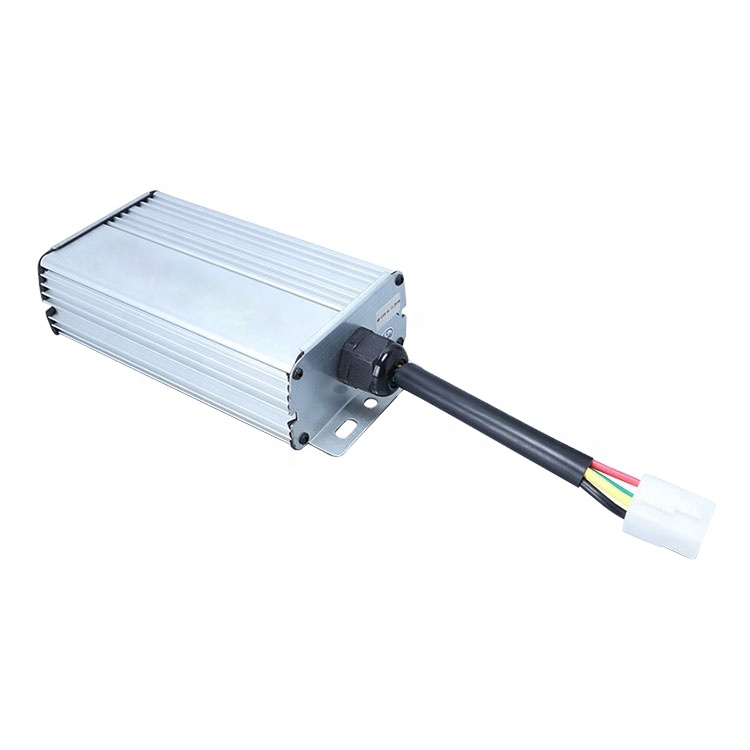
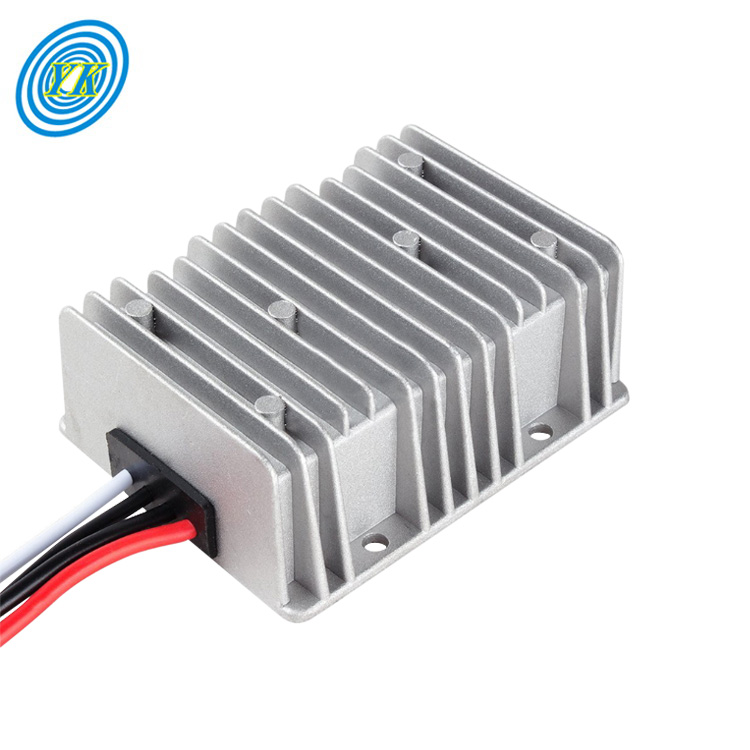
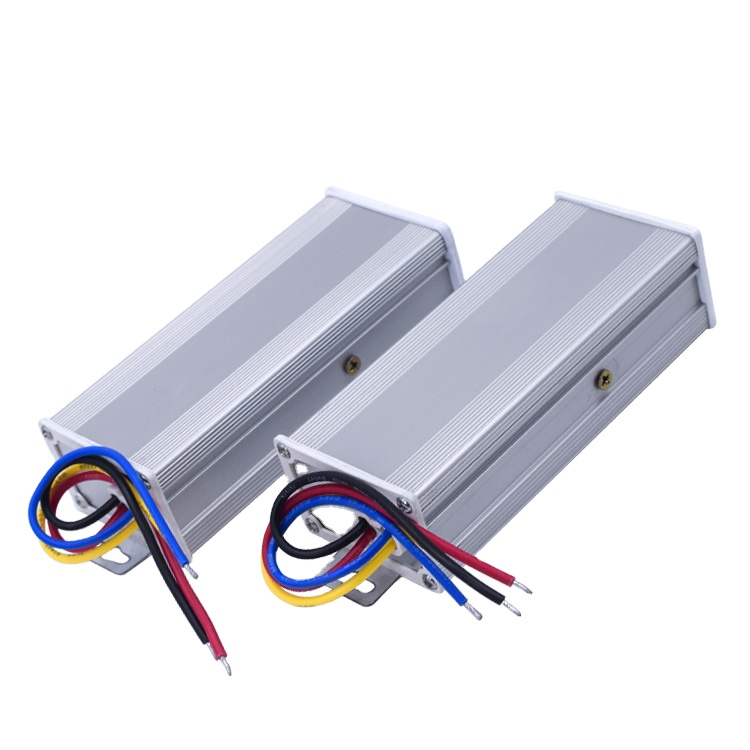
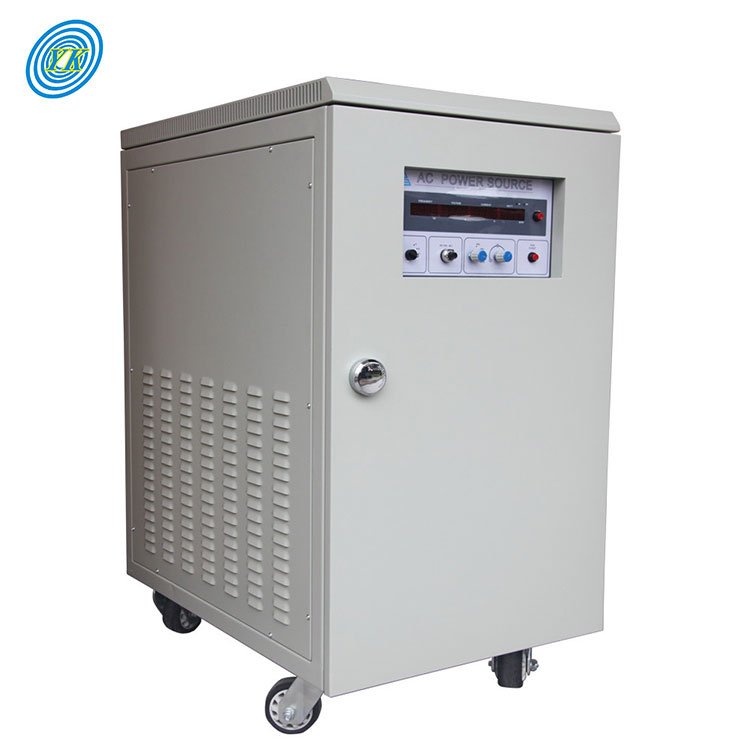
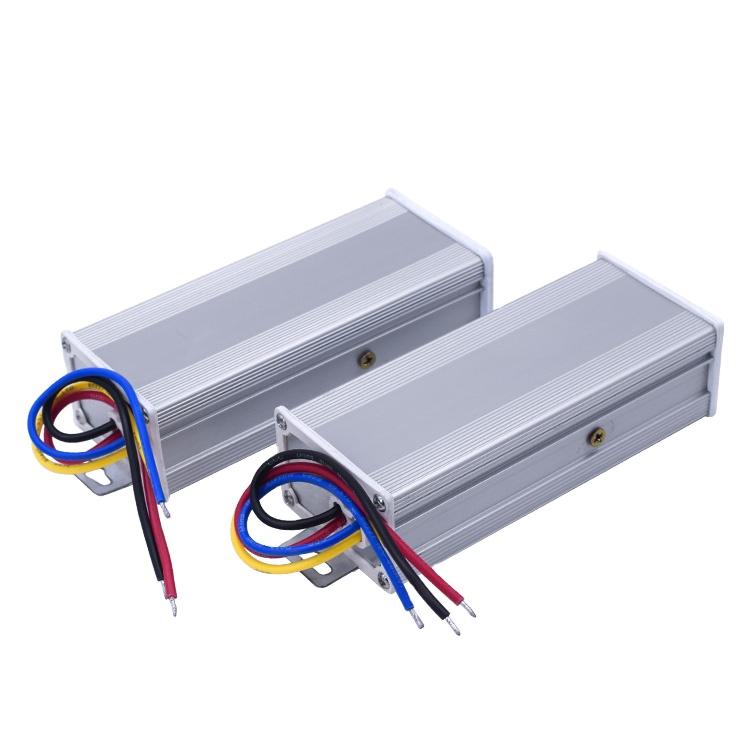
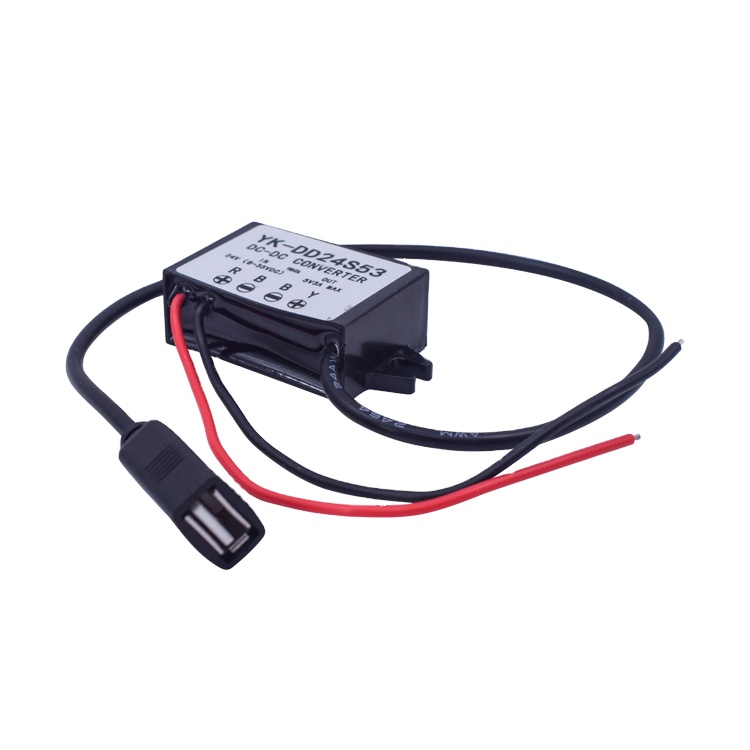
Featured Power Conversion Units & Industrial Assemblies
Precision-engineered in our ISO 9001:2015 accredited facility. All models undergo rigorous 100% full-load thermal burn-in testing to ensure uninterrupted operation across demanding Alpine temperature profiles.

23+
Years Design & OEM Heritage
10+
Precision SMT & Assembly Lines
1,229m²
SGS Onsite Audited Facility
100%
Full-Load Thermal Burn-in
Factory-Direct Advantage
Why Austrian Procurement Heads & System Integrators Partner with Varnix
Combining competitive Shenzhen/Guangdong production scale with strict European engineering standards (ÖVE, CE, EN 50155, EN 62368-1). We minimize supply chain friction with factory direct pricing and end-to-end testing.
ISO 9001:2015 & SGS Verified Quality
Every single power unit is constructed according to zero-defect manufacturing standards. Our physical workshop, assembly machinery, testing facilities, and labor safety protocols have been inspected and verified on-site by SGS Group.
Full OEM / ODM Design Agility
From customized Euro-chassis rack form factors (1U, 2U, 3U, 19-inch/ETSI) and adjustable bus voltages (12V, 24V, 48V, 110V, 220V) to CAN-bus, Modbus-RTU, and SNMPv3 telemetry interfaces, our engineering team adapts circuits to your exact bill of materials.
Direct European & Austrian Logistics
We provide full DDP (Delivered Duty Paid) door-to-door delivery right to your facility in Innsbruck, Hall in Tirol, or the wider Austrian DACH territory, handling customs clearance, EU declaration of conformity, and tariff compliance smoothly.
Engineering Whitepaper
Designing Resilient Rack Mount Power Supplies for Innsbruck's High-Altitude Alpine Ecosystem
An in-depth technical analysis for electrical engineers, system architects, and technical procurement teams deploying mission-critical DC & AC conversion equipment in Western Austria.
1. Alpine Environmental Stressors: Altitude Derating & Dielectric Strength
Innsbruck, seated in the Inn Valley at an altitude of approximately 574 meters above sea level, is ringed by high alpine infrastructure ranging from 1,000 meters to well above 2,300 meters (such as the Nordkette cable railway systems, Hafelekar weather monitoring stations, and Alpine cellular repeaters). Conventional power electronics engineered solely for sea-level conditions suffer premature degradation when installed in high-altitude environments due to reduced atmospheric pressure.
At high elevations, air density decreases, resulting in two fundamental engineering challenges that our custom rack-mount solutions directly address:
- Thermal Dissipation Degradation: Lower air density diminishes convective cooling efficiency. For rack-mounted rectifiers operating at altitudes exceeding 1,000 meters, convective heat transfer coefficients decrease by roughly 8% to 11% per 1,000 meters. Without intelligent thermal management, power semiconductors (MOSFETs, IGBTs, synchronous rectifiers) experience thermal runaway. Varnix mitigates this by designing systems with high-headroom thermal sinks and dual ball-bearing PWM fan arrays calibrated for low ambient pressure.
- Paschen's Law & Creepage/Clearance Derating: In accordance with IEC 60664-1 and EN 62368-1, the dielectric breakdown voltage of air drops systematically at altitudes between 1,000m and 3,000m. Standard commercial power supplies designed with tight clearance distances risk high-voltage flashover and insulation failure. Varnix incorporates widened clearance distances (>6.3mm on primary-to-secondary boundaries) and vacuum-impregnated isolation transformers rated up to 3,000VAC, preventing corona discharge during atmospheric pressure drops common in Tyrolean alpine storms.
2. Extreme Sub-Zero Cold Start & Rapid Condensation Resilience
Equipment deployed in external trackside enclosures, cableway machinery halls, and telecommunications towers across Tyrol frequently encounters winter ambient temperatures plummeting to -25°C or lower. Standard aluminum electrolytic capacitors utilize liquid electrolytes that freeze under such conditions, triggering massive equivalent series resistance (ESR) spikes, voltage ripple instability, and failure of the power supply to boot up (cold-start failure).
To overcome this, Varnix specifies ultra-low-temperature solid polymer capacitors and automotive-grade Rubycon/Nichicon capacitors formulated to maintain nominal capacitance at -40°C. In addition, our circuit boards receive multi-layer conformal coating (MIL-I-46058C compliant acrylic or silicone resin) that protects copper traces against microscopic condensation cycling caused by warm alpine Föhn winds suddenly sweeping through cold server cabinets.
3. Specification Matrix: Commercial Grade vs. Varnix Alpine-Industrial Grade
Selecting the right rack-mount power supply topology requires balancing total cost of ownership (TCO) against system uptime. The following matrix illustrates the performance differentials between commodity consumer-grade power supplies and Varnix industrial rack architectures:
| Technical Characteristic | Standard Commercial Rack Unit | Varnix Alpine-Industrial Rack Series | Impact on Innsbruck Deployments |
|---|---|---|---|
| Altitude Rating | 0 to 1,000 m (Unrated above) | Up to 3,500 m without manual derating | Guarantees safety in Nordkette & mountain facilities |
| Operating Ambient Temp | 0°C to +40°C | -25°C to +70°C (Hot-swappable derating) | Immune to unheated cabinet freeze & summer heat |
| Dielectric Withstand Test | 1,500 VAC Primary-Secondary | 3,000 VAC Isolation Barrier | Withstands mountain-ridge lightning electromagnetic spikes |
| Power Factor (PFC) | Passive / APFC > 0.90 | Active PFC > 0.99 (EN 61000-3-2 Cl. A) | Reduces reactive power penalties on Austrian energy grids |
| Mean Time Between Failures | < 80,000 Hours (Commercial) | > 250,000 Hours @ 40°C (MIL-HDBK-217F) | Dramatically minimizes expensive alpine helicopter service dispatches |
| Harmonic Distortion (THD) | THD < 8% | Pure Sine Wave THD < 3% Linear Load | Prevents interference in sensitive scientific & telecom circuits |
4. Innsbruck Industrial Application Blueprints
Our power conversion systems are purposefully engineered to interface with Tyrol’s high-precision industrial sectors:
- Alpine Cableways, Funiculars & Mountain Rail: Mountain transit control cabinets require isolated DC-DC step-down converters (such as our 72V/48V to 24V units) to supply redundant PLCs, safety sensors, track transponders, and brake interlock systems from main battery backup banks.
- Renewable Hydro & Solar Infiltration: Tyrol’s intensive small-hydroelectric turbines and distributed solar installations produce variable DC voltages. Varnix buck-boost converters and high-capacity chargers ensure clean, regulated DC bus delivery into central battery banks, insulating downstream telecom monitoring equipment.
- Telecommunication Towers & Fiber-Optic Hubs: Centralized 48VDC embedded rectifier systems and 19-inch rack-mount pure sine wave inverters power continuous transmission without waveform distortion, complying with strict ETSI standards.
- University of Innsbruck Research Laboratories: High-precision variable DC power supplies offering ultra-low ripple (<1mV RMS) support advanced physics, chemical synthesis, and semiconductor automation testing benches.
Factory Quality Systems
End-to-End Factory Production & Inspection Protocols
Inside our audited facility, every power conversion module advances through a 5-tier quality gate system before export boxing, ensuring failure rates remain strictly below 0.15% over the equipment lifespan.
1. Component Screening
Incoming inspection (IQC) verifies all imported MOSFETs, magnetic cores, capacitors, and microcontrollers against authorized vendor lists. X-ray inspection detects internal semiconductor die defects.
2. Automated SMT & DIP
Dual-lane Yamaha surface-mount technology machines place passive and active elements with sub-micron precision. Optical Inspection (AOI) inspects 100% of solder bridge joints and component polarity.
3. Full Thermal Burn-in
Every assembled power module is locked into dedicated environmental burn-in racks for 8 to 24 hours under 100% continuous resistive/electronic load, weeding out infant mortality defects.
4. Safety & Waveform QC
Hi-pot insulation testers check high-voltage galvanic breakdown. Digital storage oscilloscopes verify Total Harmonic Distortion (THD), ripple noise peaks, and instantaneous short-circuit recovery.
Procurement Intelligence
Frequently Asked Questions by Innsbruck Technical Purchasing Managers
Clear answers regarding compliance, electrical safety standards, minimum order quantities, and factory customization capabilities.
Are your rack mount power supplies compliant with Austrian and European electrical standards?
Yes. Our power equipment is designed in strict compliance with the European Low Voltage Directive (LVD 2014/35/EU), Electromagnetic Compatibility Directive (EMC 2014/30/EU), and RoHS Directive 2011/65/EU. Harmonized testing conforms to EN 62368-1 (Audio/video, information and communication technology equipment safety), EN 55032 Class B (EMC emissions), and EN 55035 (EMC immunity). Full test reports, CE Declarations of Conformity (DoC), and component safety documentation are provided with shipment dispatches.
How do you manage freight logistics and customs clearance into Innsbruck, Austria?
We offer complete DDP (Delivered Duty Paid), CIF, or FOB shipment terms. For rapid turnarounds and samples, express air courier (DHL, FedEx, UPS) reaches Innsbruck Airport or regional logistics depots within 4 to 6 business days. For container-load volume procurement, sea-rail intermodal routes (via European ports such as Hamburg or Rotterdam and railed to Austria) or direct China-Europe Railway Express links offer optimized freight economics. We supply all commercial invoices, packing lists, and HS code declarations for hassle-free Austrian Zollamt clearance.
Can your factory modify standard catalog units for custom 1U/2U rack dimensions or special terminal blocks?
Absolutely. Custom engineering is a cornerstone of our manufacturing operation. We routinely modify chassis depth to accommodate shallow outdoor communication cabinets (e.g., 250mm or 300mm rack depths), engineer dual-redundant hot-swappable backplanes, configure front-access Phoenix Contact terminal blocks, and program internal microcontrollers for custom over-voltage/under-voltage trip points to match specific Austrian alpine automation projects.
What is your standard Minimum Order Quantity (MOQ) and production lead time?
For standard catalog products (such as pure sine wave inverters and standard DC-DC buck/boost converters), MOQ begins from just 1 to 5 units for testing and pilot evaluations. For full custom OEM/ODM production runs involving custom silkscreen branding, specialized voltages, or unique enclosure stampings, production MOQs typically range from 20 to 50 sets. Sample units ship in 7 to 10 days, while volume factory production batches are completed within 18 to 25 business days.
How does Varnix handle after-sales service and warranty claims for overseas customers?
We back our products with a robust 24 to 36-month factory warranty directly under contract. In the rare event of a component failure, our technical engineering support team is available 24/7 via direct live chat, email, or video call to troubleshoot the issue. When a warranty defect is confirmed, replacement modular boards or entirely new replacement units are air-freighted immediately without waiting for the defective unit to be returned to China.
Ready to Engineer Your High-Reliability Alpine Power Architecture?
Discuss your technical specifications, rack dimensions, input/output voltage needs, and batch volumes directly with our senior power electronics engineering team.
Contact Us